
Technology
Replacing hexavalent chromium
TripleHard® is a patented nickel and trivalent chromium (Cr(III)) coating developed to take the place of Cr(VI) hard chrome in industrial production.
- 900–1050 HV
- hardness, no heat treatment
- 1000 h
- neutral salt spray, rating 10, depends on the nickel underlayer
- 20–40 µm
- typical on hydraulic rods, 5–10 µm on valve stems
- Cr(III)
- hard-chrome process: no chromic acid in the bath
Hard chrome plating has one unresolved problem. The chemistry that makes it work is carcinogenic, and European regulation is closing around it.
TripleHard® is a patented nickel and trivalent chromium (Cr(III)) coating, developed by Savroc in Kuopio, Finland, to take its place in industrial production. Not a laboratory alternative, and not a compromise on performance: 900–1050 HV hardness, rating 10 at 1000 h in neutral salt spray depending on the nickel underlayer, excellent wear resistance, from a Cr(III) hard-chrome process.
Why hexavalent chromium has to be replaced
Hard chrome plating is the electrolytic deposition of a hard chromium layer on steel parts that have to resist wear and corrosion: cylinder rods, valve stems, shafts, rolls. The conventional process uses hexavalent chromium, Cr(VI): chromium in its +6 oxidation state, handled in the bath as chromic acid. Hard chrome earned its place. It is hard, it resists wear and corrosion, the process is simple and inexpensive, and a century of practice has made it predictable. That is why it is still the industry default, and nothing on this page argues with its performance. The problem is not the coating. It is the chemistry during plating, and that problem is growing, not shrinking.
It is carcinogenic. Cr(VI) compounds are classified as carcinogenic, mutagenic and toxic. They are Substances of Very High Concern under REACH. The exposure risk is not confined to the bath: it extends through handling, maintenance, waste treatment and the supply chain around the process.
It is expensive to contain. A Cr(VI) line needs fume scrubbing, dedicated exhaust air treatment and complex wastewater handling. Those systems exist to manage a hazard, not to improve the coating. Every one of them is capital and operating cost attached to the chemistry rather than to the product, and the proposed EU restriction could raise that bar further.
It is a growing supply-chain risk. OEMs are removing Cr(VI) from their specifications, and the regulation below tightens every year. A supplier who still depends on it is increasingly answering questions about continuity rather than about quality.
Under REACH, the principle is that substances of this kind are progressively replaced by safer alternatives wherever a technically and economically viable one exists. TripleHard® was built to be that alternative.
Where the regulation stands
Position as of October 2026. Regulatory processes move; verify against ECHA before relying on a date.
Cr(VI) compounds currently sit on Annex XIV of REACH, the Authorisation List. Using them lawfully means working under an authorisation: your own, or one granted upstream in your supply chain that covers your use and its conditions, with the notification duties that follow. Either way it is tied to a review period, with the cost and administrative load that carries.
That is changing. The European Commission asked ECHA to prepare a restriction report to move these substances from Annex XIV to Annex XVII, the Restriction List. The difference matters: authorisation is a controlled permission to continue, restriction is a prohibition with defined exemptions.
The process so far:
| When | What |
|---|---|
| 11 April 2025 | ECHA submitted the restriction proposal, covering 13 hexavalent chromium compounds (made public on 29 April 2025) |
| 2026 | RAC (Committee for Risk Assessment) adopted its final opinion |
| 11 June 2026 | SEAC (Committee for Socio-Economic Analysis) agreed its draft opinion |
| 17 June – 19 August 2026 | Public consultation on the draft SEAC opinion |
| Expected November 2026 | Final SEAC opinion, after an extension of the opinion timeline under REACH Article 71(3) |
| After that | European Commission and Member States review, before any restriction enters Annex XVII |
Sources: ECHA, Authorisation List (Annex XIV) and restrictions under consideration.
- ECHA submits the restriction proposal
Thirteen hexavalent chromium compounds proposed for Annex XVII, the Restriction List. The process starts.
- RAC adopts its final opinion
The Committee for Risk Assessment confirms the health case. The first of the two committee opinions.
- SEAC agrees its draft opinion
The Committee for Socio-Economic Analysis weighs costs and benefits; a draft, not yet a decision.
- Public consultation
Industry and other stakeholders comment on the draft SEAC opinion.
- Where the process stands today
- Final SEAC opinion
The last committee step. Timeline extended under REACH Article 71(3).
- Commission and Member States decide
If adopted, the substances move to Annex XVII: authorisation becomes prohibition with defined exemptions.
Dates from ECHA. The final SEAC opinion and the Commission decision are expected steps, not published ones.
What it could mean for coaters, OEMs and the market
The final conditions are not yet decided, so what follows are possible consequences of the proposal as it stands, not certainties.
For coating plants. As proposed, the restriction does not ban hard chrome plating on metal. It would allow it within limits for worker exposure and annual caps on Cr(VI) releases to air and water, after an 18-month transition. How strict the worker limit will be is still open. The proposal sets out two variants for plating on metal: 5 µg/m³, the same as today's EU binding limit, or 1 µg/m³, five times lower. ECHA's Committee for Risk Assessment (RAC) has proposed a single, stricter limit of 0.1 µg/m³. The draft opinion of the Committee for Socio-Economic Analysis (SEAC, June 2026) considers the 1 µg/m³ variant likely proportionate, notes that a single limit of 0.5 µg/m³ could also be appropriate, and considers 0.1 µg/m³ likely not proportionate with an 18-month transition. In ECHA's survey of 685 companies using Cr(VI) substances, 31 % said they would not yet meet a 1 µg/m³ limit; most of them intended to invest in further controls, and 6 % of all respondents expected to close or relocate. For many plants the stricter variant would therefore likely mean further investment in enclosure, extraction, monitoring and wastewater treatment, and ECHA's impact assessment counts closures and relocations among the expected costs (ECHA webinar on the restriction proposal, 18 June 2025; RAC opinion and draft SEAC opinion, June 2026).
For OEMs and their buyers. If some plants cannot meet the limits, the supplier base for Cr(VI) hard chrome in Europe could become smaller and more concentrated, and part of the capacity could move outside the EU, lengthening supply chains. Qualifying a replacement coating typically takes years, longer than the proposed transition period.
For the market. Higher compliance costs and reduced capacity could lead to higher prices and longer lead times for Cr(VI) hard chrome in Europe. Regulation is moving in the same direction elsewhere: in the United States, EPA has tightened emission standards for chromium electroplating and banned PFOS-based fume suppressants.
For a buyer, the question may be less whether Cr(VI) plating stays legal than whether the supplier base it depends on will still be there, on today's terms, in five years. The direction is settled even though the final text is not, and moving late is likely to cost more than moving early.
That qualification timeline is the reason to start now. Obtaining first test results alone can take up to six months, and the full path from first customer contact to complete approval runs from three to five years, sometimes seven.
Why earlier trivalent chromium did not work
Trivalent chromium, Cr(III), is chromium in its +3 oxidation state: far less toxic than Cr(VI), and not new. Decorative Cr(III) plating has existed for decades. The reason it never replaced Cr(VI) hard chrome in industrial use is simple: it did not withstand wear.
Earlier trivalent coatings were softer, adhered less reliably, and degraded under the sliding and impact loads that hard chrome exists to survive. They were also harder to run: trivalent chemistry is process-sensitive, and bath stability, bath lifetime and repeatable quality were the recurring failure points at production scale.
Two changes make TripleHard® different.
A nickel anchor layer. The coating is not a single Cr(III) film on bare steel. A nickel layer is deposited first, and the chromium layer builds on it. The result is adhesion that survives mechanical abuse rather than adhesion that survives a lab test.
A carbon-containing chromium structure. The Cr(III) layer is formulated so that its hardness holds under heat instead of falling away, and so that the coating resists acid attack rather than dissolving in it. Both are measured below.
The work behind this was long. Development began in 2013. The formulation came partly from an observation that basic trivalent chromium was sometimes tougher than it should have been under apparently unchanged conditions, and the research that followed was an effort to find out why, and then to control it.
The coating
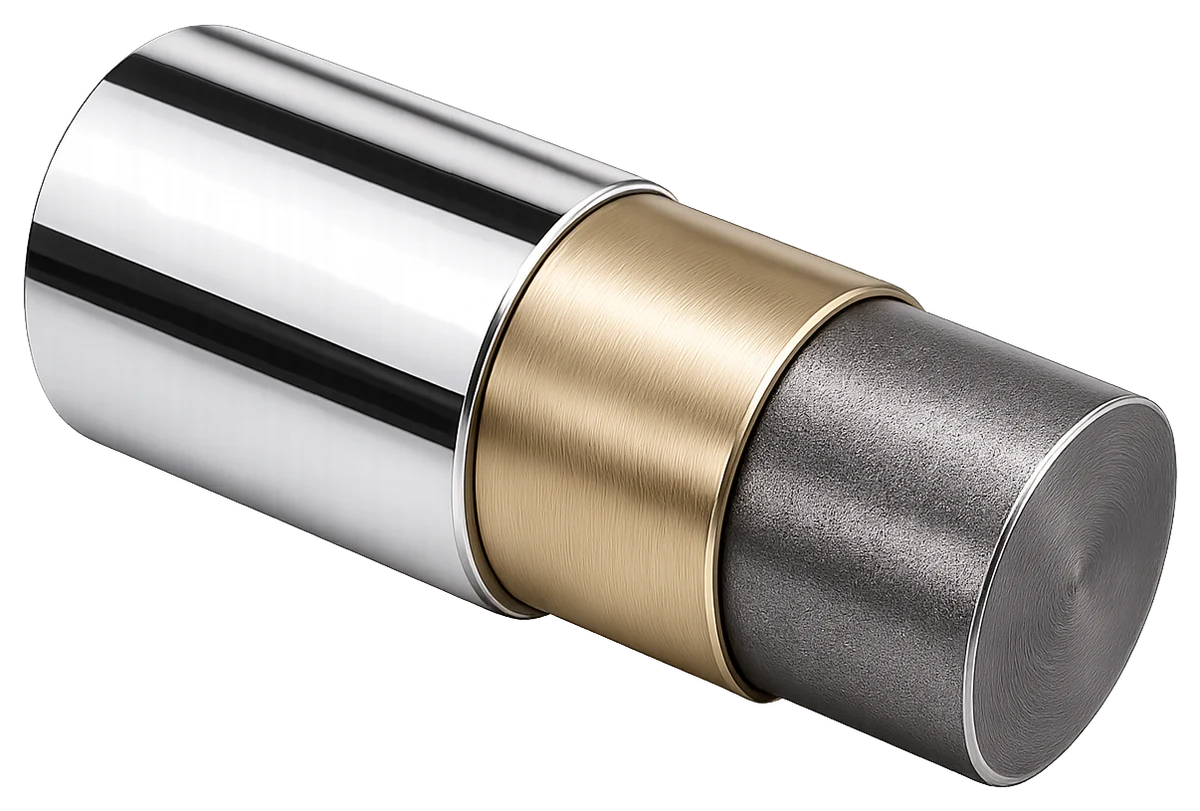
- TripleHard® Cr(III) layer
- Nickel anchor layer
- Steel core
Illustration of the layer structure, not to scale.
| Property | TripleHard® |
|---|---|
| Chemistry | Nickel and trivalent chromium (Cr(III)). No chromic acid, no boric acid |
| Hardness | 900–1050 HV, full hardness without post-plating heat treatment |
| Structure | Nickel anchor layer with one or more Cr(III) layers above it. The continuous line deposits several Cr(III) layers in one pass |
| Typical thickness | Typically 20–40 µm on hydraulic cylinder rods and 5–10 µm on engine valve stems; set per application during qualification |
| Adhesion | No peeling or flaking after bend, indentation and aggressive scratch testing |
| Heat behaviour | Hardness maintained, and increases, after heat cycles to 500 °C |
| Surface finish | Can be ground and polished to the same Ra/Rz targets as hard chrome |
| Compatibility | Established on base materials including Ck45 and 20MnV6 |
| Regulatory | A Cr(III) hard-chrome process: no chromium trioxide or chromic acid in the bath, the Cr(VI) substances that need REACH authorisation |
Thickness is set per application during qualification. Where a drawing specifies a hard chrome thickness, TripleHard® can be deposited to match it, so existing fits and grinding allowances can stay.
Measured performance
Every figure below comes with the test that produced it. Where a comparison is made, the comparator is conventional Cr(VI) hard chrome tested alongside. The coating has been validated by a major global OEM, and has been in industrial production at Hydroline in Tampere, Finland, since 2024.
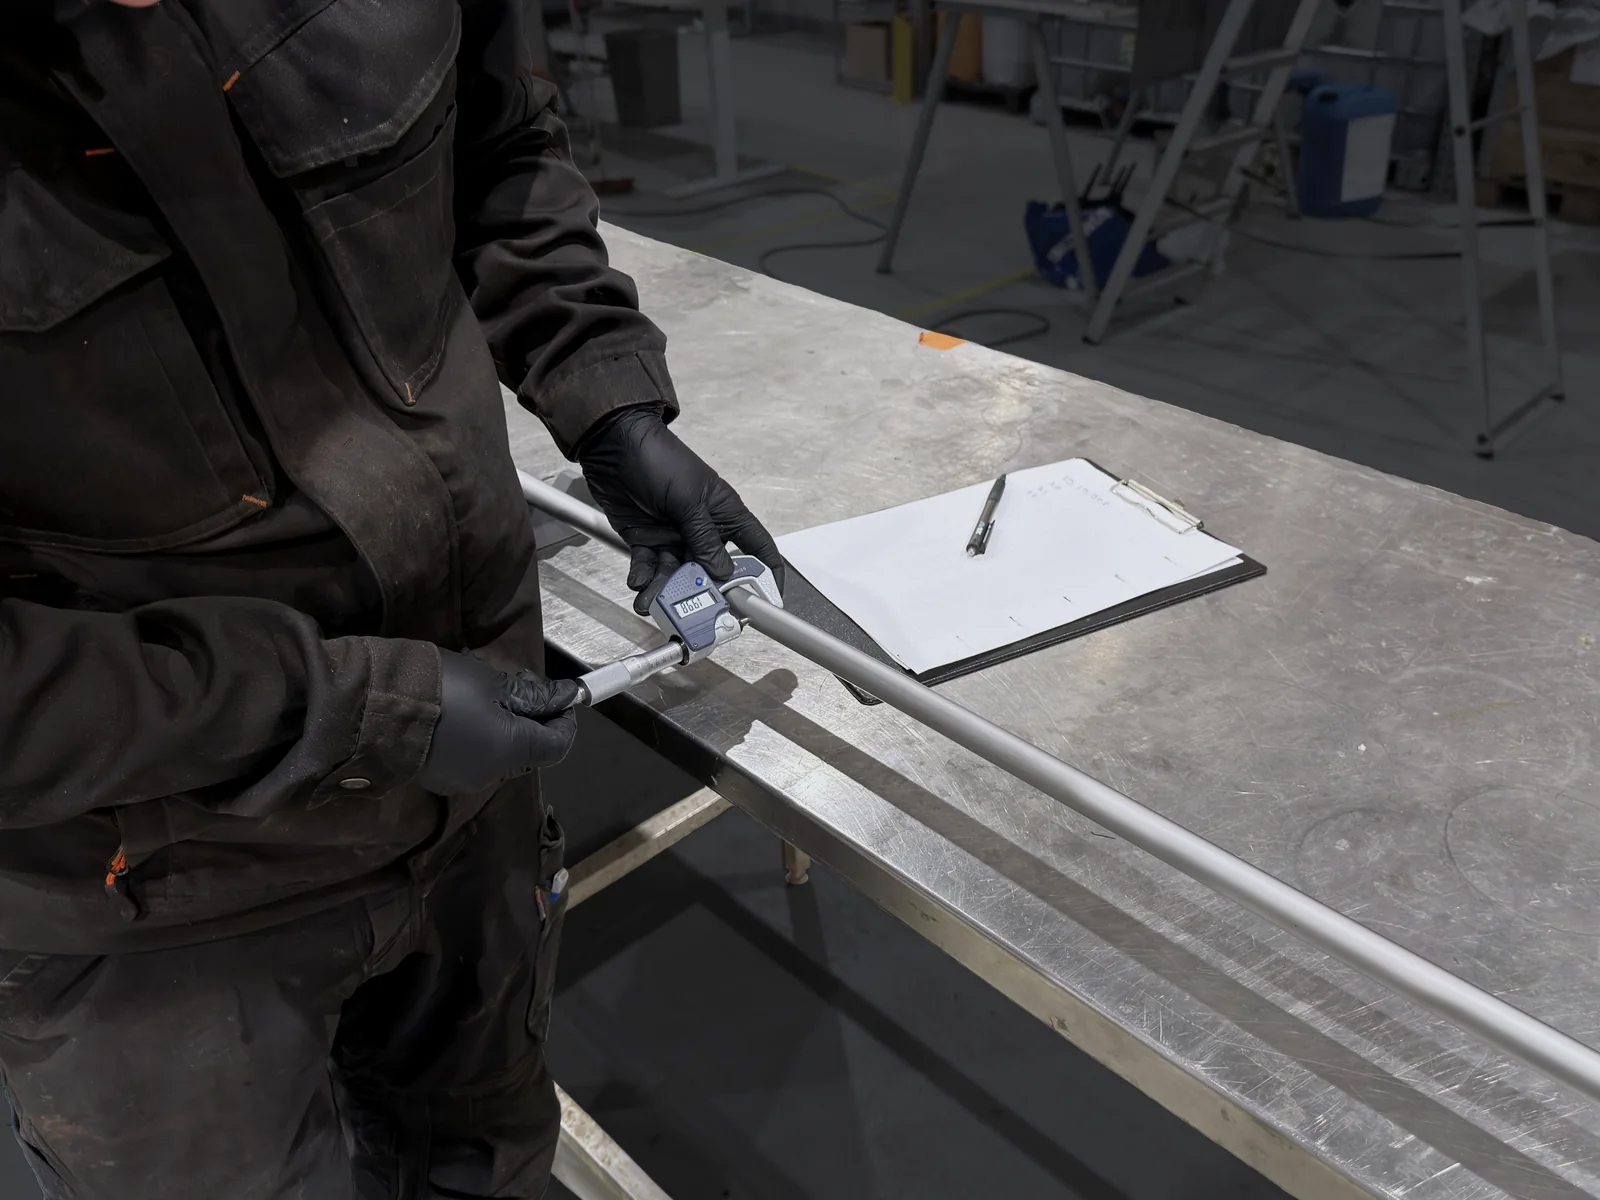
Acid resistance
Benchmarked against two conventional hard chrome coatings in 5 % H₂SO₄ at 100 °C. The hard chrome samples were taken out when the attack was visible; the TripleHard® sample ran the full 23 minutes. The TripleHard® sample was heat-treated after plating and the Cr(VI) hard chrome samples were not: the test simulates the high-temperature service of an engine valve. On a valve the heat treatment is not a separate step, because the engine runs the valve at around 500 °C.
| Sample | Time in acid | Corrosion depth | Mass loss |
|---|---|---|---|
| Cr(VI) hard chrome, sample 1 | 22 min | 22 µm | measurable |
| Cr(VI) hard chrome, sample 2 | 2 min | 7 µm | measurable |
| TripleHard® | 23 min | 0 µm | 0 g |
This is the result that matters for exhaust-gas condensates, fuel-sulphur environments and any process where the part meets acid.
Sliding wear under extreme load
Block-on-Ring (BOR) test, 3 200 seconds (53 minutes).
| Sample | Outcome |
|---|---|
| Cr(VI) hard chrome | Galled at 1 125 lbf, with a friction spike and visible damage |
| TripleHard® | Withstood the maximum test load of 1 275 lbf, an estimated 850 MPa contact stress, with no surface failure |
Abrasion
Taber abrasion test, CS-10 wheels, 1 000 cycles, 1 kg load.
| Sample | Wear index |
|---|---|
| Cr(VI) hard chrome | 2.0 mg |
| TripleHard® | 1.03 mg |
Roughly half the material loss under the same abrasive conditions.
Surface after sliding wear
Sliding wear test, 600 cycles at contact pressures up to 20 MPa, TripleHard® at 40 µm against hard chrome at 80 µm.
| Contact pressure | TripleHard® surface roughness Ra | Cr(VI) hard chrome surface roughness Ra |
|---|---|---|
| 0–10 MPa | about 0.1–0.3 µm | about 0.1–0.3 µm |
| 15 MPa | about 0.2 µm | about 0.5 µm |
| 20 MPa | about 0.3 µm | about 1.75 µm |
At half the thickness the TripleHard® surface stayed smooth to the end of the test; the hard chrome surface roughened sharply above 15 MPa.
Behaviour at temperature
Conventional hard chrome begins to lose hardness at elevated temperature. TripleHard® does the opposite: internal testing at Savroc confirms the coating retains its integrity through heat cycles to 500 °C and exceeds its base hardness afterwards, a consequence of structural changes in the carbon-containing layer activated by heat. TripleHard® withstands more than 500 °C without softening.
Adhesion
Passed multiple mechanical stress tests, including a bend test, indentation and an aggressive scratch test, with no peeling or flaking. Under full flex and under sharp contact the coating stayed attached to the steel. Like hard chrome, the chromium layer carries a fine microcrack network, and under heavy deformation that network opens rather than the coating letting go of the part.
Corrosion
The laboratory benchmark most specifications ask for comes first. The results from service and from real media follow it, because a hard chrome replacement is finally judged on how a rod looks after months in a mine, not only on how it looks in a cabinet.
| Test | Conditions | Result |
|---|---|---|
| Neutral salt spray (NSS, ISO 9227) | 35 °C, evaluated per ISO 10289, TripleHard® over a specified nickel underlayer | Rating 10, no base metal corrosion, at 1000 h, and at 250 h and 500 h. The result depends on the nickel underlayer configuration |
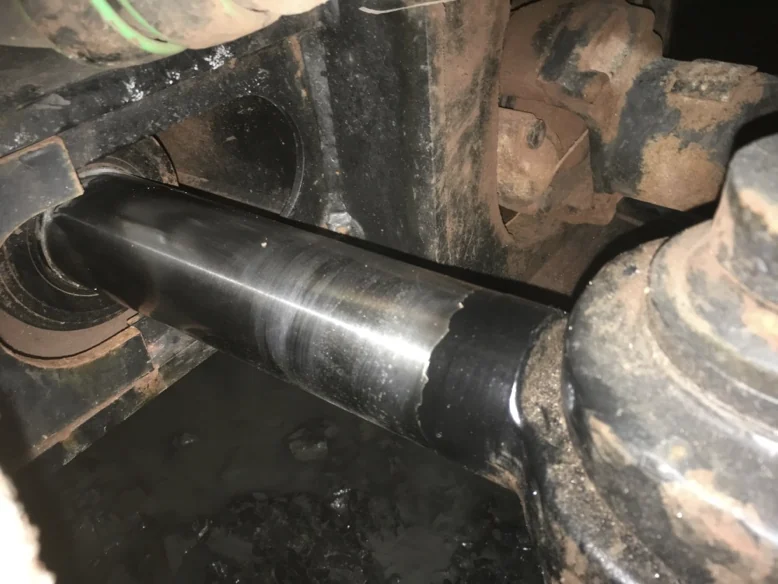
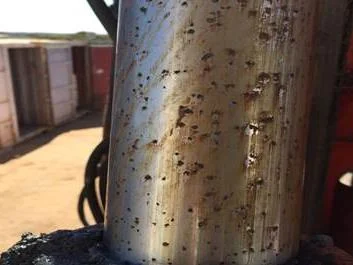
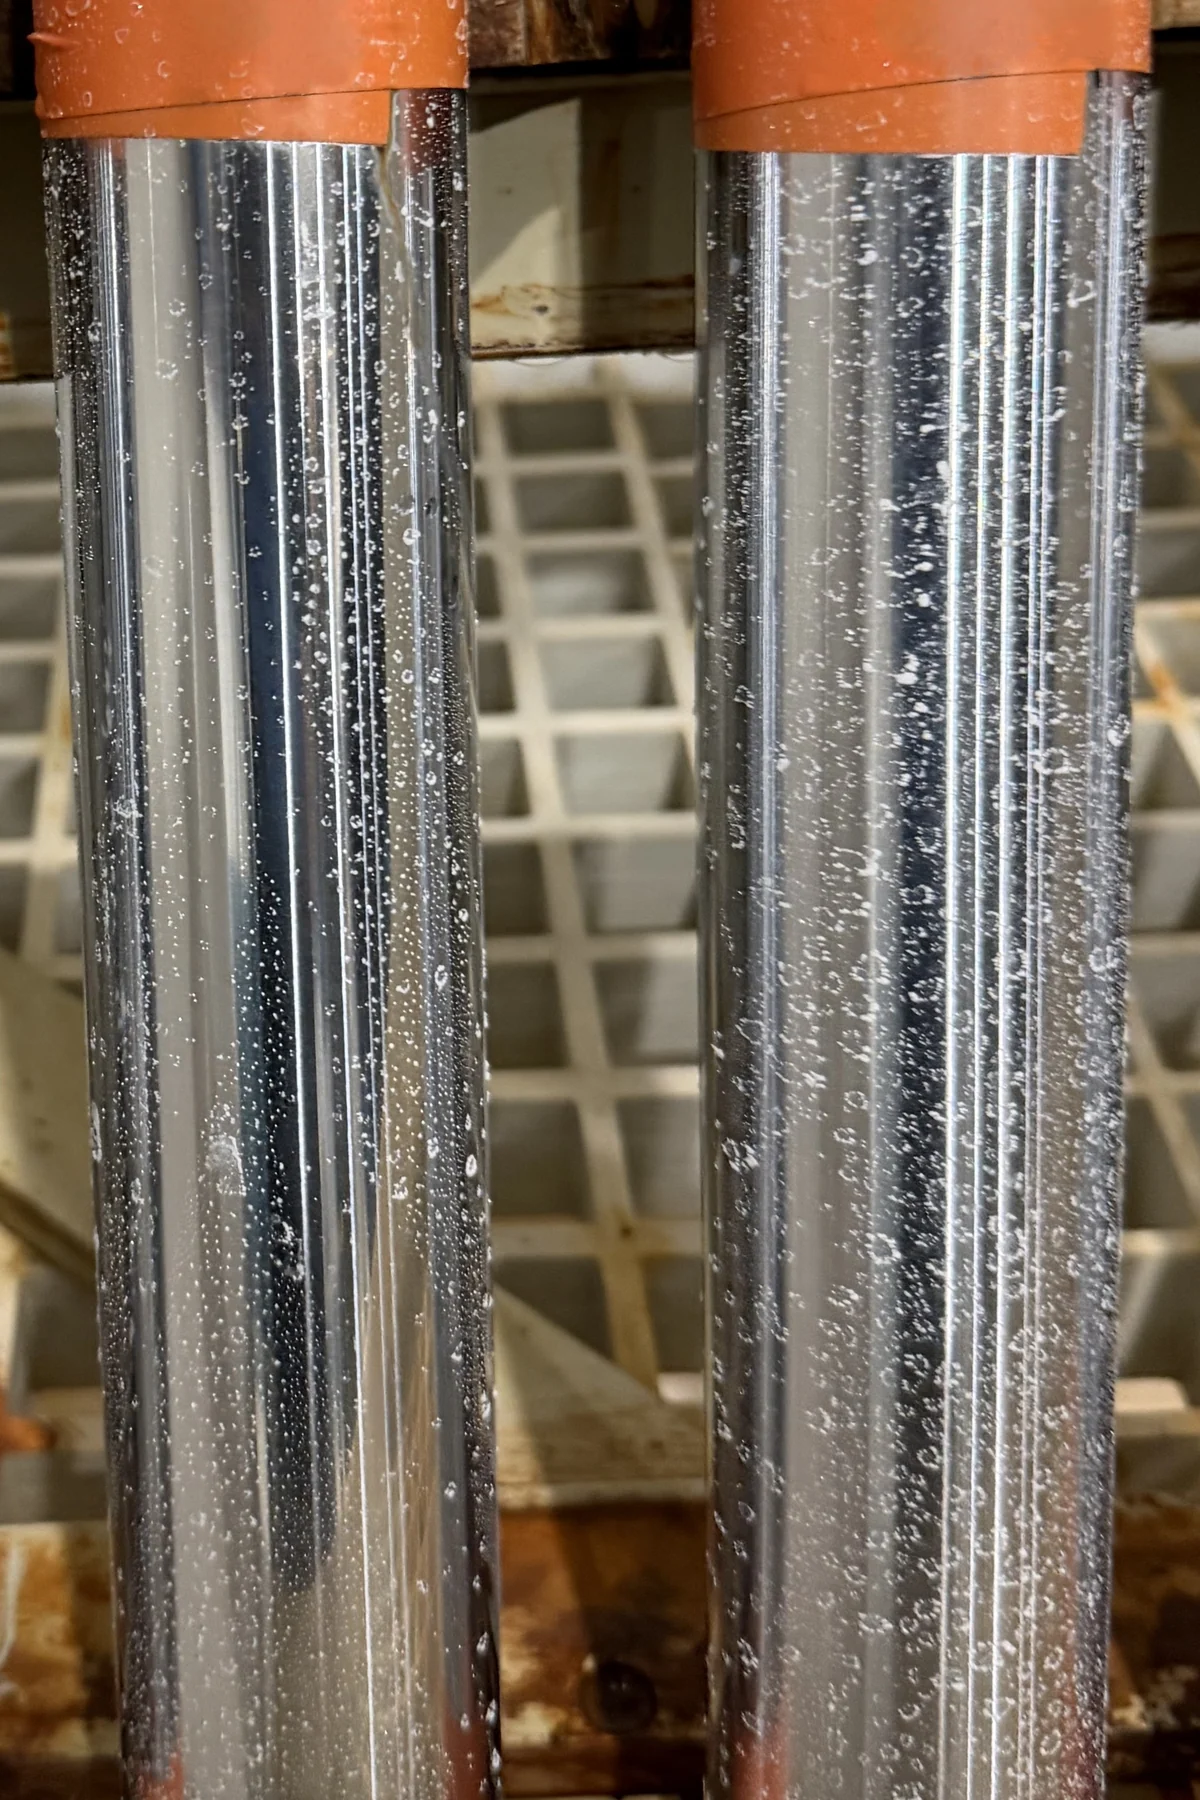
| Mine service, hydraulic cylinder rods | Australian mine, salt, high temperature | TripleHard® on ordinary 20MnV6 steel: no rust after 34 months. Cr(VI) hard chrome on the same steel was replaced at 2 months, and on AISI 329 stainless steel it rusted at 4 months: at least 17 times the service life on the same steel, in a field case with a global mining equipment OEM |
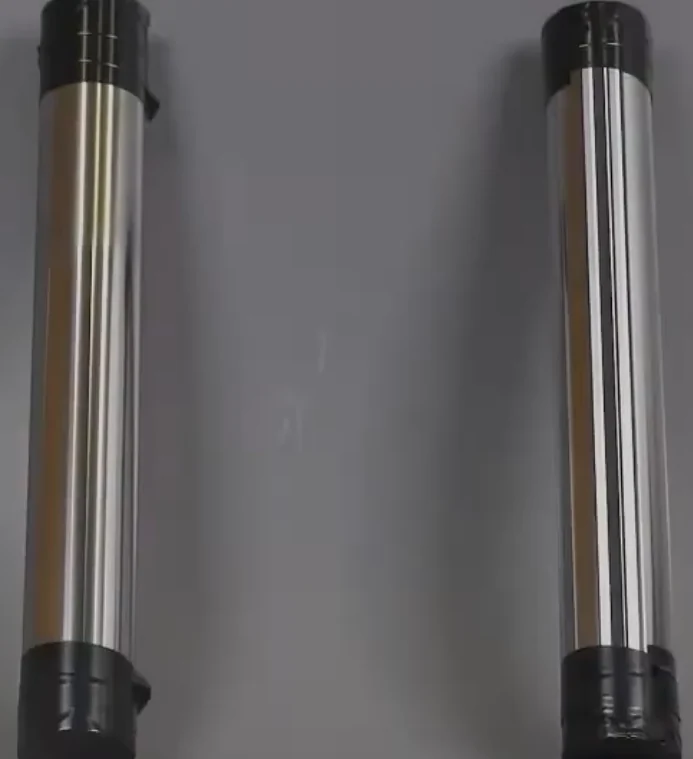
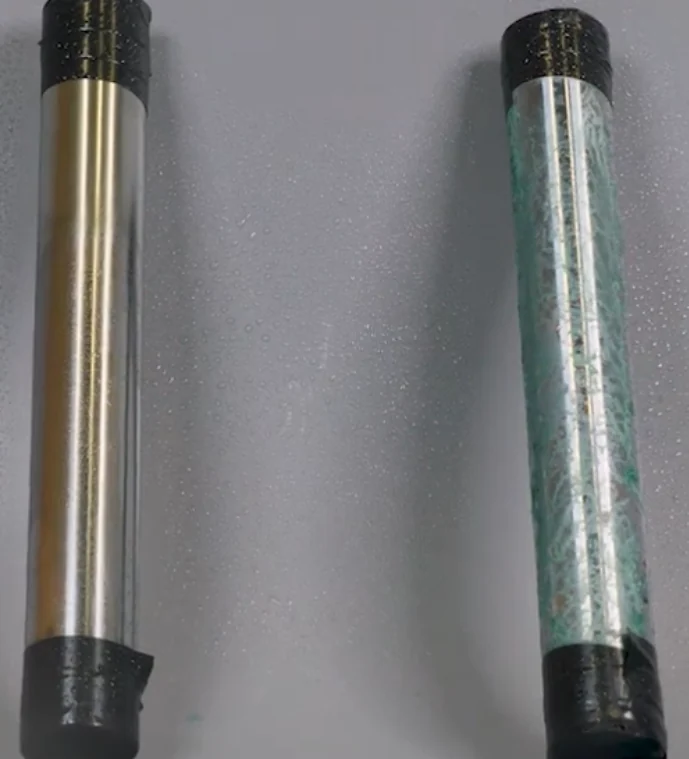
| Mine water droplet test (Hydroline) | 72 h continuous exposure to genuine mine water: pH < 1, NaCl, MgCl₂, H₂SO₄ | No visible corrosion, surface intact. The Cr(VI) sample was severely degraded and unusable |
| Ball valve in service | Strong nitric acid at 70–80 °C, electronics recycling plant | More than 1.5 years with corrosion and wear resistance intact, where hard chrome leaked and electroless nickel corroded |
| High-pressure water pump in service | Continuous operation in high-salinity water, Canada, independent case study | TripleHard® and a high-performance thermal-spray coating each reached two years of service; Cr(VI) hard chrome failed after a few months |
| Acetic acid salt spray (AASS, ISO 9227) | 20 µm TripleHard® on steel, tested to the standard | Intact at 48 h, 360 h and 456 h, when the test was stopped |
OEM specifications typically set neutral salt spray at 200–250 h; TripleHard® holds rating 10 at 1000 h, nickel underlayer dependent. The rows below it say what that means in service: a rod in a mine, a valve in hot acid, a sample in genuine mine water.
The mine, the ball valve and the shock absorber shafts are written up in full on the case studies page.
The process
TripleHard® is an electrolytic process built on familiar plating principles. That is deliberate. The chemistry is new; the operating model is not.
The four stages
- Surface preparation
- Etching
- Nickel deposition
- TripleHard® Cr(III) layers
Rinsing between stages prevents carry-over between baths. On the continuous line the four stages run in one enclosed pass; on a converted open-tank line they are four baths.
What the process requires
Whichever route the coating is produced by, trivalent chemistry imposes real constraints. Getting them wrong is the usual cause of an unstable bath.
| Element | Requirement |
|---|---|
| Plating tanks | Titanium, titanium with HDPE lining, HDPE or PP (polypropylene) |
| Steel near the bath | Minimise. Steel corrodes and contaminates the chromium bath |
| Zinc and copper | Harmful to the trivalent process. Avoid near the bath |
| Anodes | Graphite or Ti-MMO (titanium mixed metal oxide) |
| Rectifiers | Standard equipment is sufficient |
| Ventilation | Standard ventilation. The chromium content of a trivalent bath is many times lower than that of a Cr(VI) bath, so the ventilation and wastewater treatment it needs are much smaller |
| Process control | Trivalent chromium is process-sensitive. Continuous monitoring is a requirement for stable production, not an optional extra |
The ventilation point carries real money with it. A Cr(VI) line has to filter and purify its process fumes and exhaust air, and treat its wastewater. With many times less chromium in the bath, a trivalent line needs much less of both.
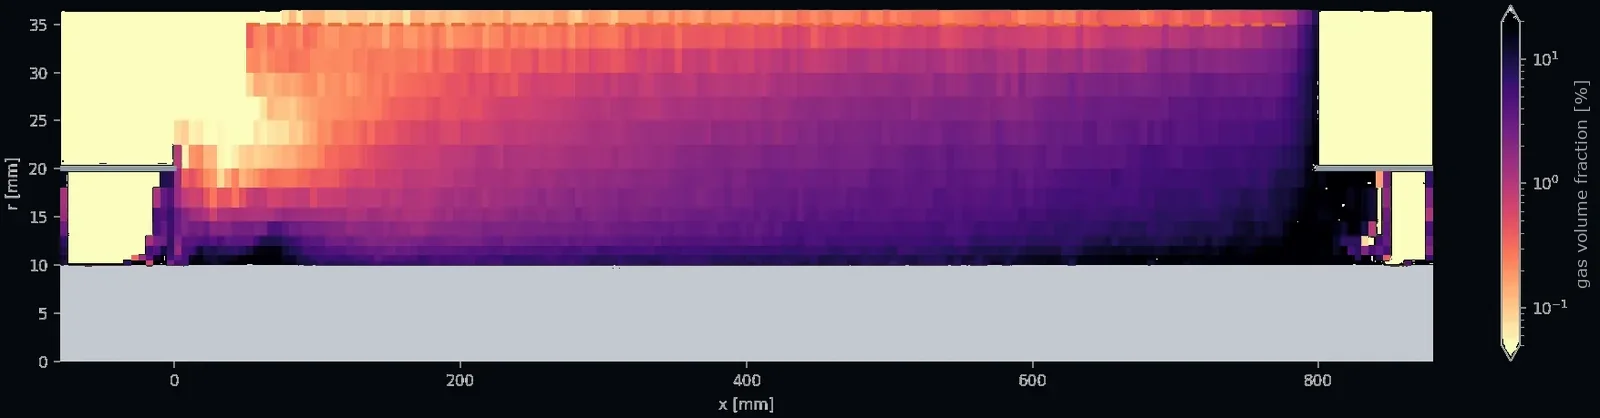
Process sensitivity is handled by design, not by habit. Trivalent plating evolves hydrogen at the part, and where the flow is weak the gas gathers and the deposit suffers. On the continuous line every cell is modelled before it is built: electrolyte flow, gas and the current field in one model, so the inlet geometry is chosen for the rod, not inherited from an open tank. How the modelling works.
Two routes to production
TripleHard® reaches parts two different ways, and which one applies depends on the component.
1 A new continuous line, for hydraulic cylinder rods
This is Savroc's focus. The continuous line is not a conversion of anything: it is a complete new production line, built by our industrial equipment partner to Savroc's process design, and the customer orders it from them. Nickel and trivalent chromium are applied in a single enclosed pass, at 3.5 times the throughput of batch plating at equal floor area, by Savroc's own measurement on the Kuopio prototype in October 2026. The industrial-scale prototype has run in Kuopio since August 2026; production ramp-up with a rod manufacturer is the target for H1 2027, and mass production on the continuous line is planned for 2027.
Read more: The Line · Hydraulics · Engineering · Industrial partners
2 Converting an existing line, for engine valves, shock absorber rods and open-tank work
Most of the existing infrastructure carries over. The Cr(VI) bath is replaced with a TripleHard® Cr(III) bath, a nickel bath is added where the line has none, anodes are changed to graphite or Ti-MMO, and housekeeping keeps zinc and copper away from the process. Standard ventilation is usually sufficient. This is the secondary route, and the one that makes TripleHard® available without a capital project.
Read more: Engine valves · Shock absorbers · Working with Savroc
Compared with the alternatives
Replacing Cr(VI) at industrial scale takes more than regulatory compliance. An alternative has to clear three bars at once: performance, scalability and cost structure.
| Route | Primary limitation | Where TripleHard® differs |
|---|---|---|
| Cr(VI) hard chrome | Carcinogenic exposure, authorisation cost and administrative load, and limited long-term availability as the restriction advances | A Cr(III) hard-chrome process by design: no chromium trioxide to authorise, at industrial performance |
| Thermal spray / PVD | High capital expenditure, energy-intensive, and poorly suited to high-volume serial production of long components | Electroplating, which keeps it inside serial-manufacturing economics. Runs either as a new continuous line or on converted existing equipment |
| Other Cr(III) chemistries | At hard-chrome thickness, typically limited by bath lifetime, process stability and heavy-duty wear performance | Engineered for industrial bath stability, repeatable quality and heavy-duty applications |
Frequently asked questions
Is the TripleHard® process REACH-compliant?
TripleHard® is a Cr(III) hard-chrome process: a trivalent chromium electrolyte with REACH-compliant additives. There is no chromium trioxide, chromic acid or boric acid in the bath, so the REACH authorisation that Cr(VI) plating needs does not apply to it, and audits are simpler.
Do we still need post-plating heat treatment?
For most applications, no. TripleHard® reaches full hardness without post-plating heat treatment, which shortens lead time, simplifies the process and reduces energy use. A hydrogen-embrittlement relief bake protects the base material, not the coating: whether it is needed depends on the steel and on the customer's requirement.
Do we have to change component design or tolerances?
In most cases, no. TripleHard® is an electroplated coating with a similar dimensional impact to hard chrome, so existing designs and fits can usually be kept. It can match existing hard chrome thickness, or use a thinner layer with an adjusted grinding allowance.
Is it compatible with our existing seals and surface roughness targets?
Usually. TripleHard® is engineered for seal-friendly surfaces and can be finished to the same Ra/Rz targets as hard chrome, and recommended grinding and polishing guidelines are provided. Seal performance depends on the seal design and the operating conditions, so it is confirmed for your seal system in the project.
Do we still need field trials?
Less than you might expect, but qualification is still done application by application. For hydraulic cylinder rods the field references and the laboratory data exist, so your own verification can be limited to your components and duty cycles. For engine valves and shock absorber rods the application is in qualification, and the results on those pages are test results for those parts, not transferred from rods.
Is it suitable for high-temperature service?
Yes. The coating maintains its hardness and structure at elevated temperature, as demonstrated in heat cycling to 500 °C. This makes it suitable for components where conventional hard chrome softens or cracks over time.
Do we convert our existing line, or do we buy a new one?
It depends on the component. For hydraulic cylinder rods, the answer is a new line: the continuous process cannot be retrofitted into an open-tank installation, and the complete line is built and sold by our industrial equipment partner to Savroc's process design. For engine valves, shock absorber rods and other open-tank work, the answer is conversion: most of your existing infrastructure carries over. See "Two routes to production" above and Working with Savroc.
What does a coater need to change when converting an existing hard chrome line?
The Cr(VI) bath is replaced with a TripleHard® Cr(III) bath, anodes are changed to graphite or Ti-MMO, and housekeeping keeps zinc and copper away from the process. Because trivalent fumes are far less harmful, standard ventilation is usually sufficient and scrubbers are not required. Tank material matters: titanium, titanium with HDPE lining, or HDPE, with steel near the bath minimised. The nickel stage is a standard nickel-plating step.
How do we specify TripleHard® in drawings?
Ready drawing clauses and specification text are supplied, covering coating type, thickness range and surface finish. These can be added directly to your internal standard and customer documentation.
Documentation
Every datasheet, brochure and test report in one place. Page copy states hardness as 900–1050 HV; the shock absorber rods datasheet also gives the range that is tuned per application.