
The continuous line
Hard chrome in one continuous pass.
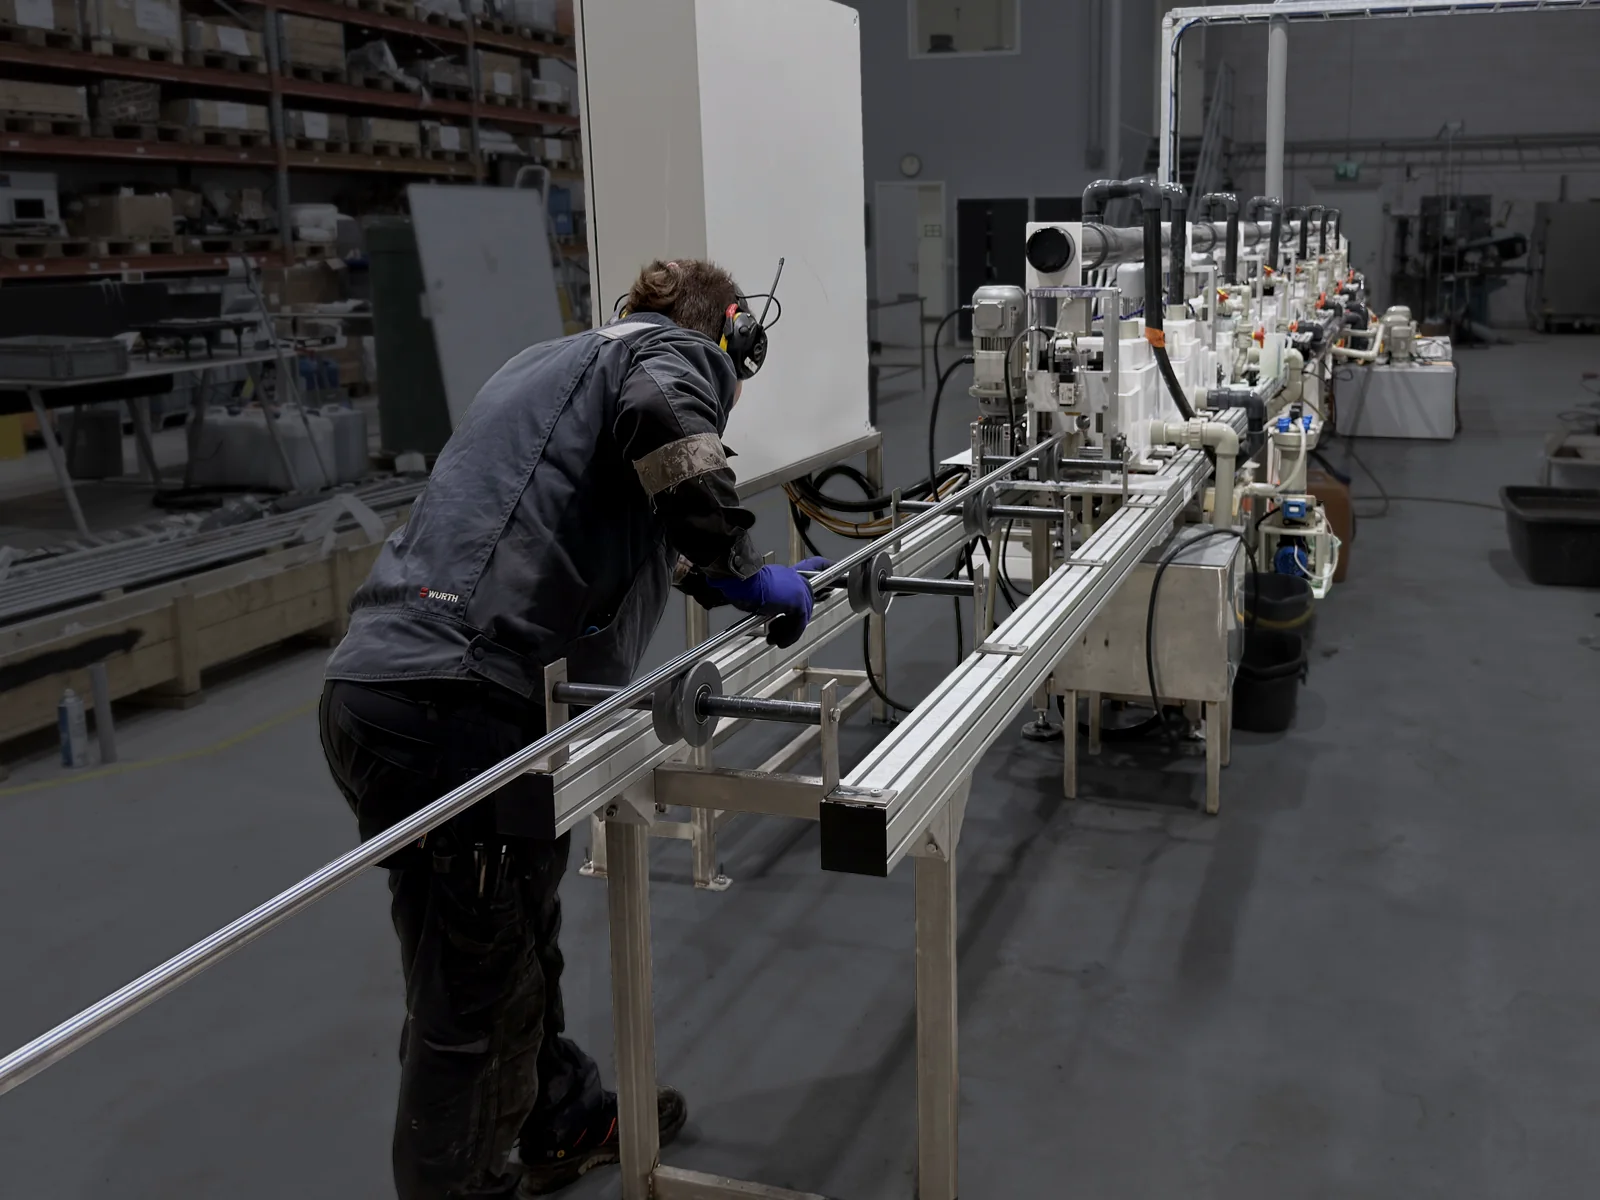
The world's first continuous production line for TripleHard®: hydraulic cylinder rods enter at one end and leave coated at the other, with no manual transfer between baths.
Four stages
From bare steel to
TripleHard®, without stopping.
1Surface preparation
Cleaned and activated, ready for the layers.
2Etching
A controlled etch opens the steel surface for the anchor layer.
3Nickel deposition
The nickel anchor layer goes on first. It bonds to the activated steel, gives TripleHard® its adhesion and carries much of its corrosion protection.
4TripleHard® Cr(III) layers
Trivalent chromium is built up over the nickel to hard-chrome-level hardness, without heat treatment. The flow along the rod keeps the layer even.
Schematic, not to scale. A rinse follows every stage.
How it differs
Traditional plating stops between every step. This line does not.
Conventional Cr(VI) hard chrome plating is a batch process: open tanks, an overhead crane, and an operator between every bath. The continuous line replaces the sequence with a single automated pass.
- 4 baths1 pass
- Surface preparation, etching, nickel and Cr(III) in one uninterrupted run
- OperatorNo contact
- No part is lifted between baths by hand, and the baths are enclosed
| Traditional plating | The continuous line |
|---|---|
| Separate work stages | One uninterrupted process |
| Open tanks | Fully enclosed system |
| Crane transfer between baths | Automated conveying |
| Fume extraction over open tanks | Vapours contained in the line |
Safe by design
Chemicals stay inside the machine.
The enclosed design keeps chemicals, mist and emissions inside the line. Dosing and handling are automated, so operators are kept away from both.
-
Operator safe.
Minimal contact with chemicals and moving parts
-
Fully enclosed.
Splash, mist and emissions contained
-
Lower footprint.
Less chemical use, less waste, no scrubbers
-
Automated handling.
Consistent dosing, consistent quality
Control and data
Smarter process. Stronger results.
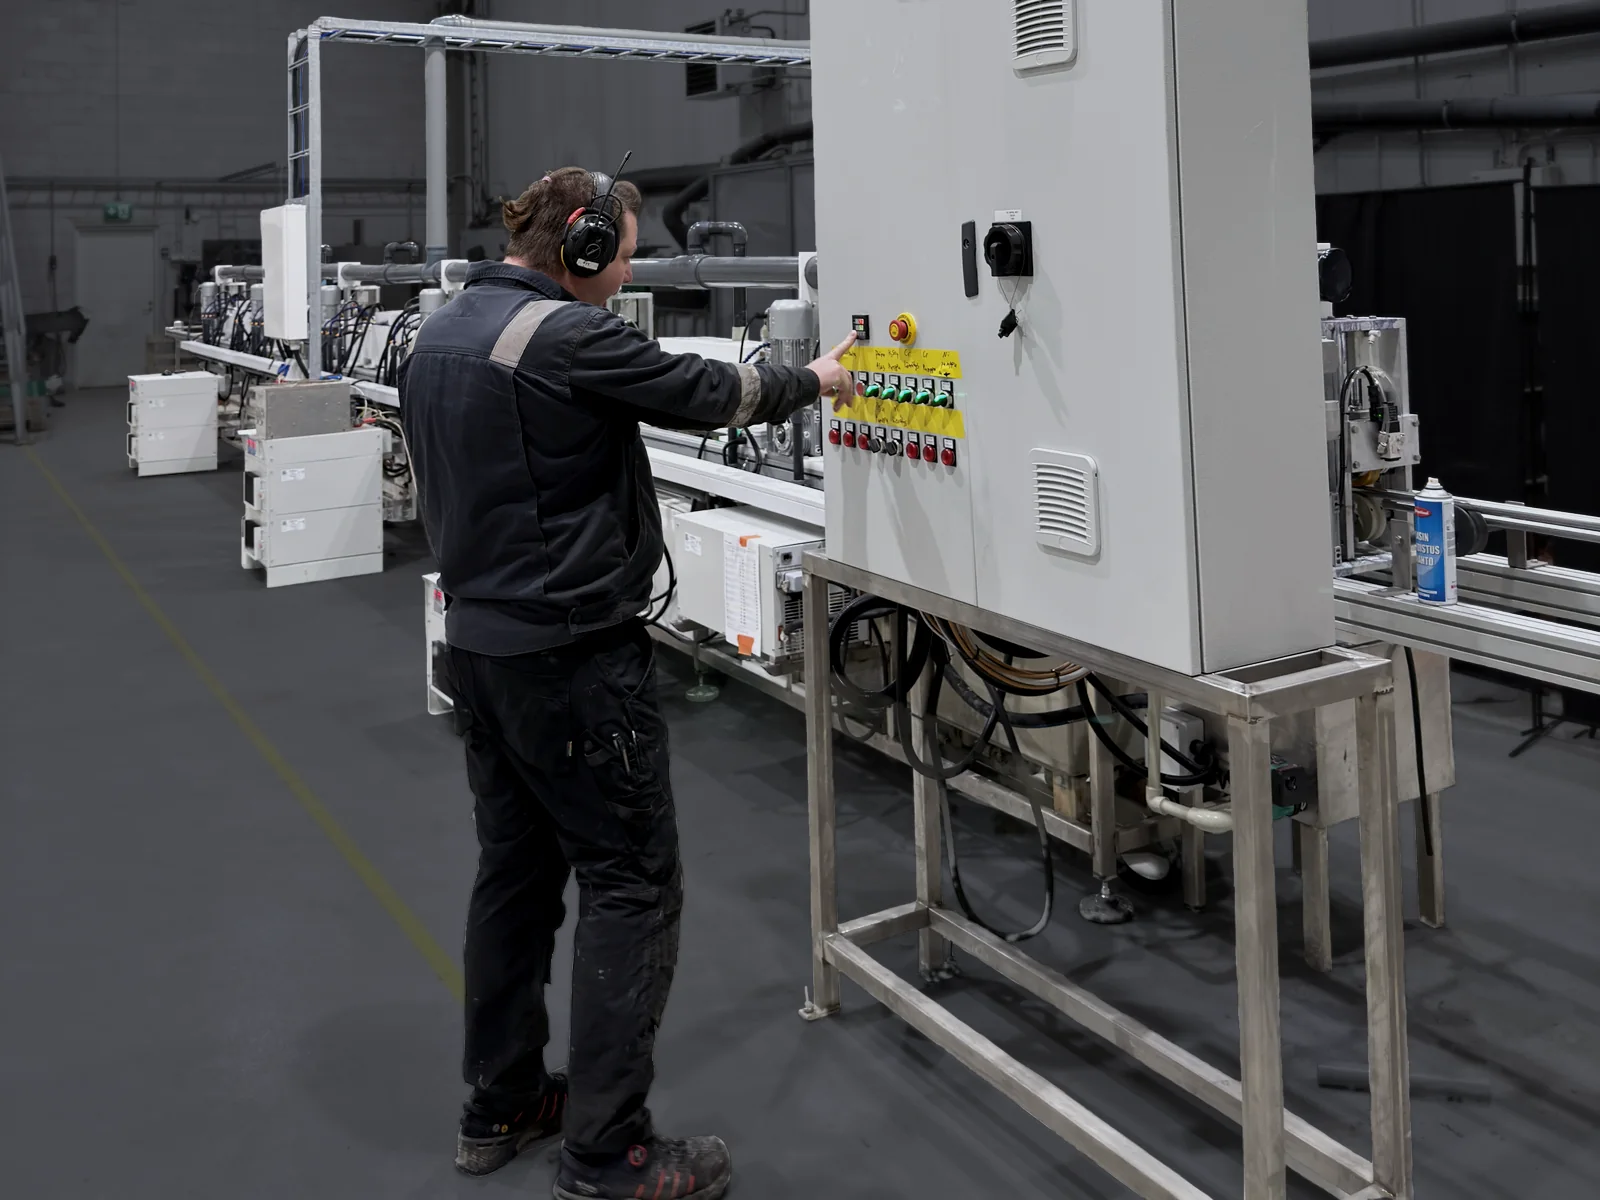
Trivalent chromium is sensitive to its process conditions, so the line is built around control. Process-control software is being developed for the continuous production line, with real-time process monitoring, alarms and part-level traceability, designed to be included with each line licence.
- Monitor. Process parameters in real time
- Alarm. Deviations flagged as they happen
- Trace. Process data for every part
From pilot to industrial scale
Built from a 3D-printed pilot in under a year.
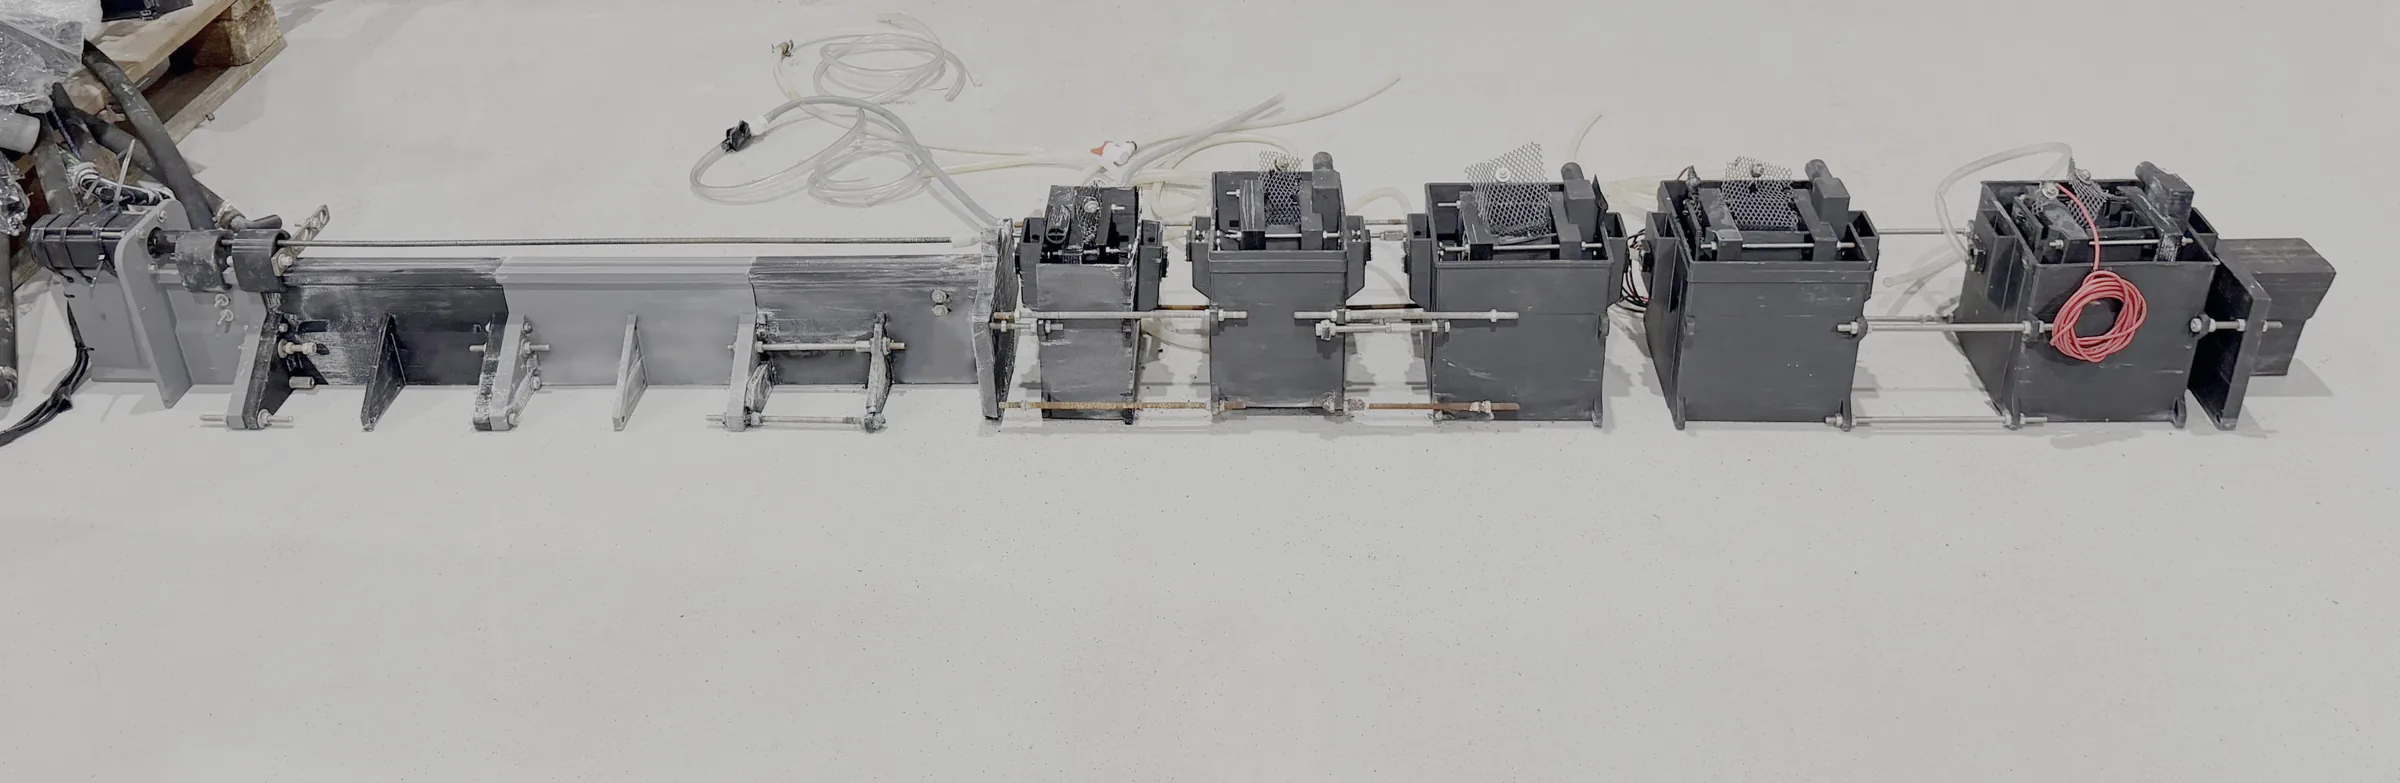
The continuous process is developed on a self-built, 3D-printed pilot line. More than 50 versions were tested over months of near-daily experiments.
The industrial-scale line arrives in Kuopio.
ILMAR completes the installation. First test runs.
First coatings produced. Results reported excellent.
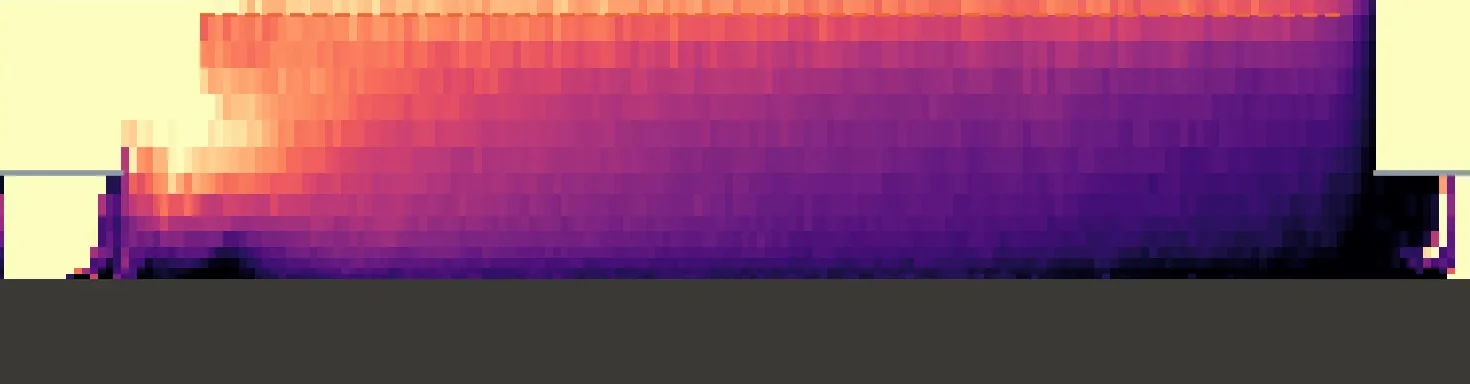
An inlet ring for the plating cell is chosen from five variants in the flow model, 3D-printed and fitted to the line.
Version 1 complete: the first-round run parameters are locked and optimisation continues.
Target: production ramp-up with a rod manufacturer.
Plan: mass production on the continuous line.
Where we are now
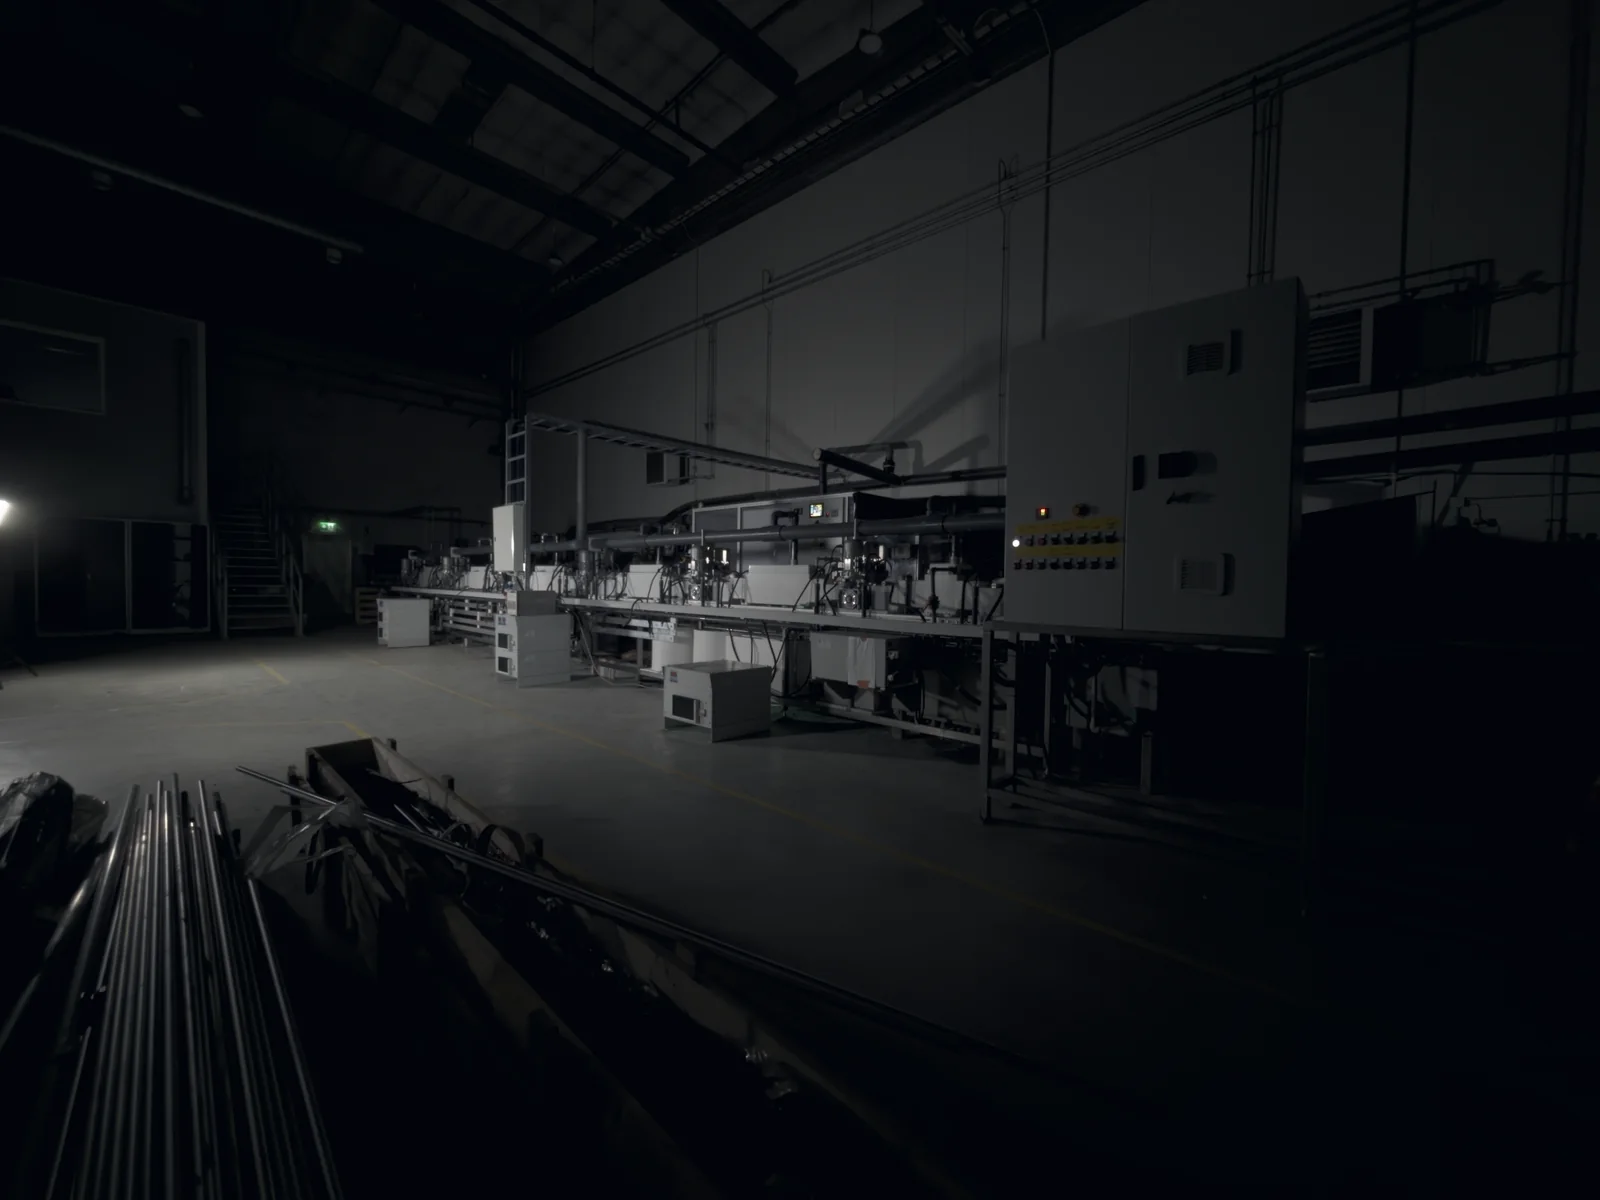
An industrial-scale prototype, running in Kuopio.
The line in Kuopio is not a line for sale. It is the industrial-scale prototype, built by ILMAR, whose job is to lock the parameters and produce the data for the lines built for customers. Version 1 is complete: the first-round run parameters are locked, and optimisation continues. By the end of 2026 Savroc will know exactly what a customer's line must be, with the playbook for replicating it; each customer line is then configured and sized for that customer in simulation. The customer does not get a copy of the Kuopio line.
Two steps follow. Target: production ramp-up with a rod manufacturer in H1 2027. Plan: mass production on the continuous line in 2027. If moving off hexavalent chromium is in your plans, this is the year to come and see it.
Who does what
Savroc designs the process. Our partner builds the line.
-
Engineering company and licensor
Savroc
Leads the project with you: simulation, the process and line design, commissioning in your plant and process support in production. Licenses TripleHard® and supplies the chemistry.
-
Built the Kuopio line
ILMAR
The industrial-scale line in Kuopio was built by ILMAR in Italy: equipment engineering, automation and manufacturing, to Savroc's process design.
-
Built for your plant
Your line
A customer line is built and delivered by an industrial equipment partner to Savroc's process design. You order the line from them; Savroc commissions the process in your plant.
See it for yourself
The line runs in Kuopio. Come and watch it coat a rod.
Bring your drawings or your parts. Jussi Räisä shows you the line, the test data and what a project in your plant would look like. No sales deck, no commitment.
Jussi Räisä, CEO jussi.raisa@savroc.com +358 44 307 1409