
Hydraulics
Reliable performance under pressure.
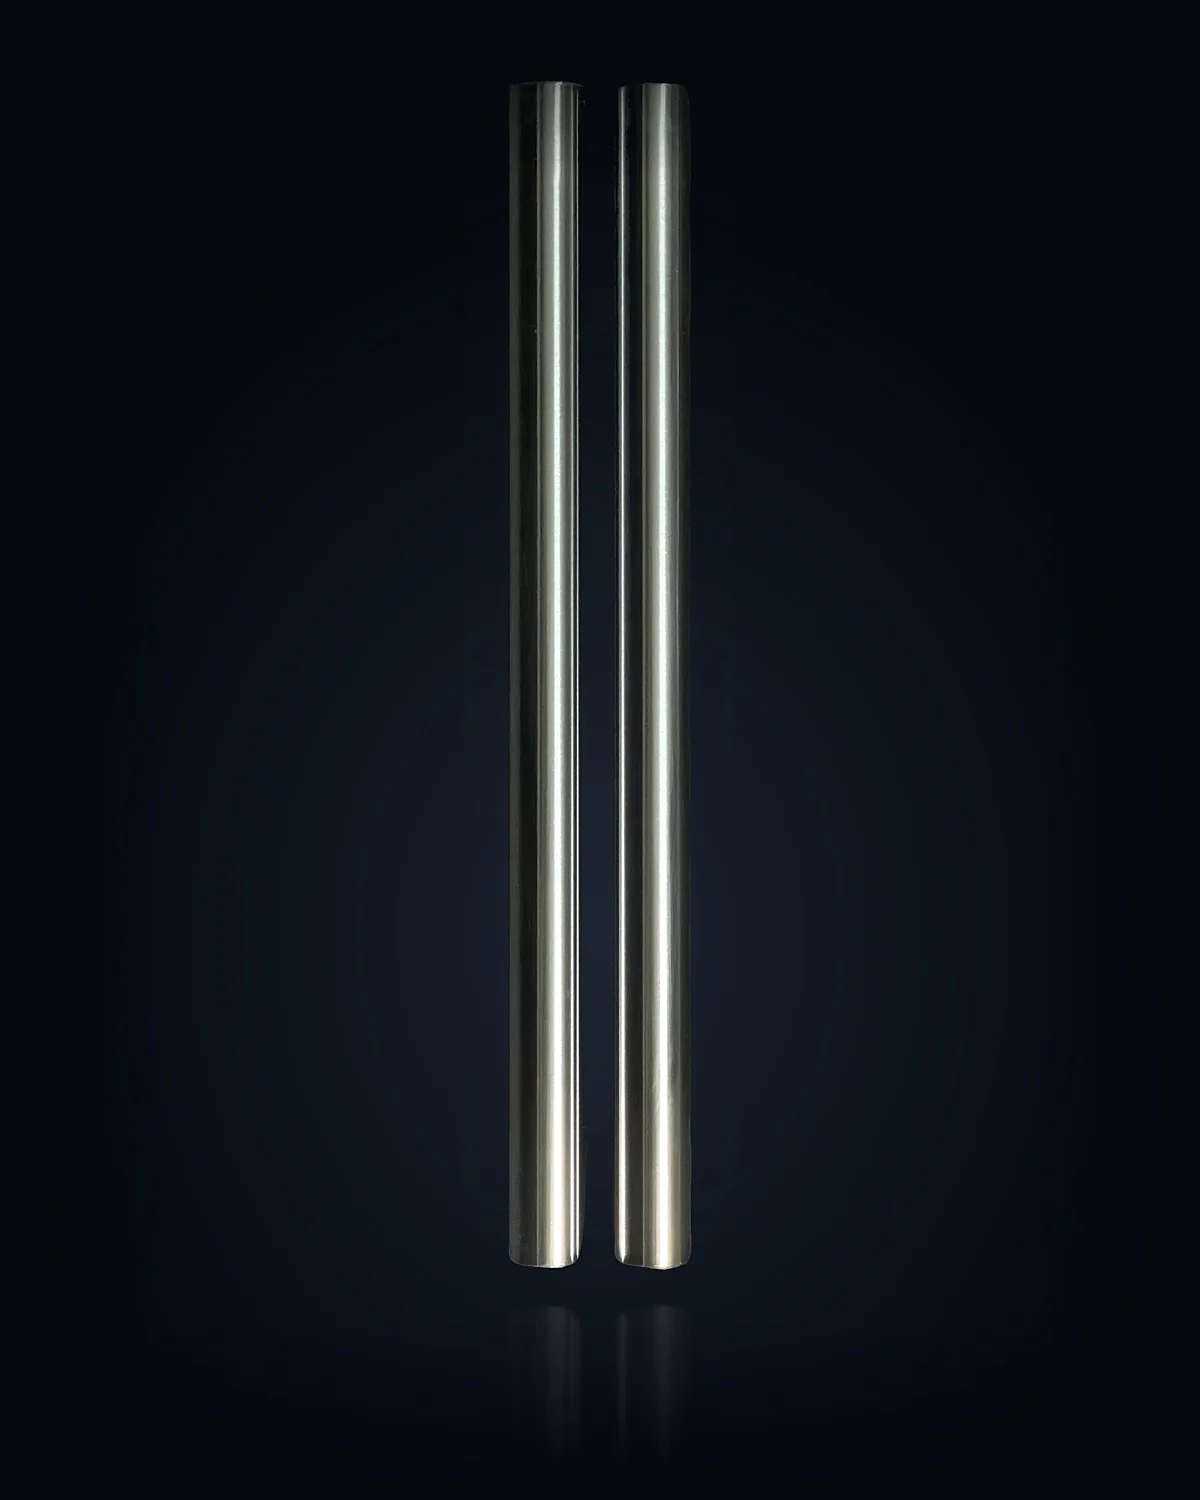
TripleHard® on hydraulic cylinder rods: hardness that resists scuffing and impact, corrosion resistance for the field, and a surface that is kind to seals. Made in a Cr(III) hard-chrome process.
- 1000 h
- neutral salt spray, rating 10, depends on the nickel underlayer
- ≥17×
- service life in the headline mining case: 34 months TripleHard®, 2 months Cr(VI) hard chrome
- 72 h
- in genuine mine water, droplet test: no corrosion
Why hydraulics
The rod is the part that meets the world.
A cylinder rod is scratched by grit, struck by rock, wetted by rain and mine water, and slid through a seal thousands of times a day. The coating has to survive all of it without damaging the seal that keeps the oil in.
- Scuffing and impact. Hard-chrome-level hardness and excellent adhesion: the coating stays on when the rod meets the rock
- Corrosion. Rating 10 at 1000 h in neutral salt spray, depending on the nickel underlayer; no rust after 34 months in mine service
- Seal-friendly surface. Low friction and a controlled finish, so seals last
- No post-plating heat treatment. Full hardness as plated
How it is produced
On the continuous line.
Achieved TripleHard® has been in industrial production since 2024 in open-tank coating of hydraulic rods at Hydroline. The continuous line has been in pilot operation in Kuopio since August 2026.
The continuous line was built for hydraulic rods: surface preparation, etching, nickel and the TripleHard® Cr(III) layers in one enclosed pass. The Kuopio line was built by ILMAR; Savroc commissions the process on every customer line.
See how the line works How a project works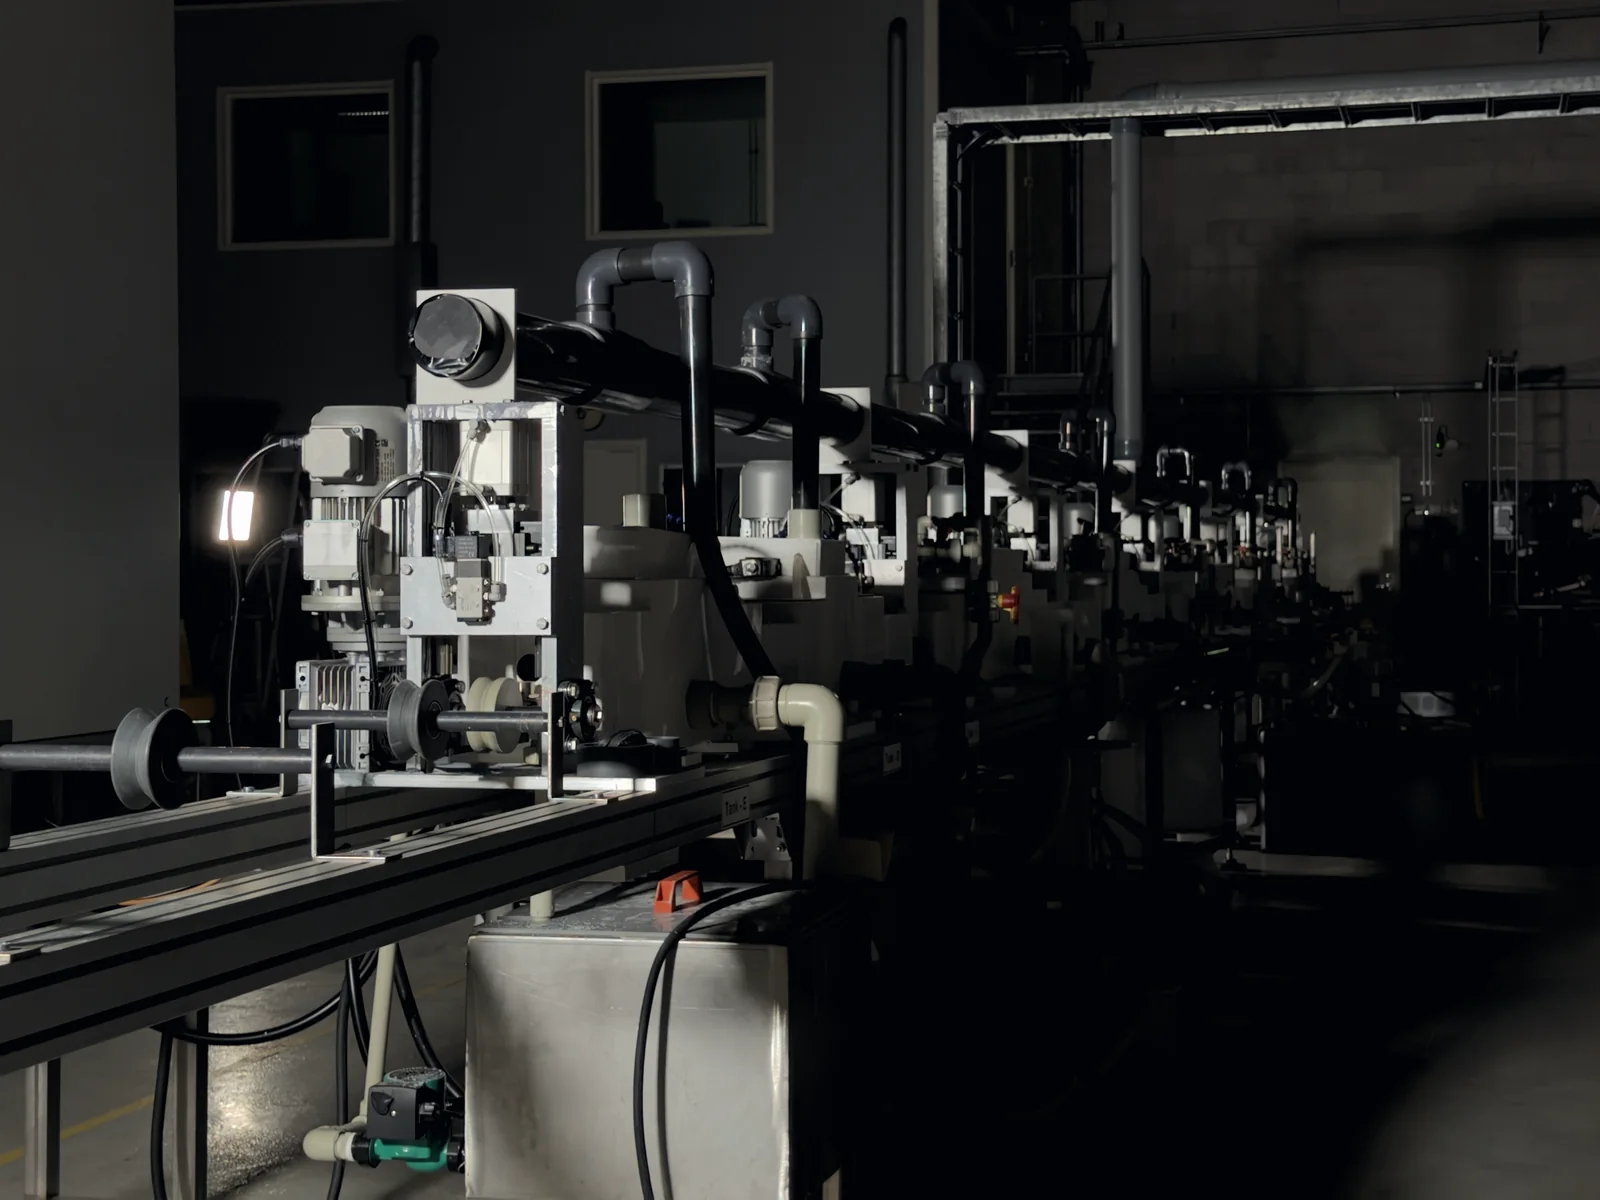
Technical package
What is measured.
Full test conditions and the regulatory position are on the technology page.
| Corrosion | NSS (ISO 9227): rating 10 at 1000 h, and at 250 and 500 h; depends on the nickel underlayer. Field: 34 months on a mining cylinder, no rust. Lab: 72 h mine-water droplet test, no corrosion |
|---|---|
| Hardness | Hard-chrome level, full hardness without heat treatment; the measured range is on the technology page |
| Coating structure | Nickel anchor layer + trivalent chromium layer |
| Base materials | Ck45, 20MnV6 and other common rod steels |
| Field durability | Long-term industrial use, including 34 months on a mining cylinder |
Corrosion in service
No rust at 34 months. Hard chrome rusted at 2.
Three rods in the same Australian mine. Cr(VI) hard chrome rusted at 2 months on ordinary 20MnV6 steel and at 4 months on AISI 329 stainless steel. TripleHard® on 20MnV6 showed no rust at 34 months.
Frequently asked questions
Does TripleHard® replace Cr(VI) hard chrome one to one on hydraulic rods?
In tested applications, yes: the same rod, the same seals, and a coating that meets or exceeds the hardness and corrosion resistance of Cr(VI) hard chrome. Each application is confirmed with you, from the simulation of your parts to commissioning, with our data behind your own OEM qualification.
How thick is the coating?
Typically 20–40 µm on hydraulic cylinder rods. The thickness depends on the application and is specified from your drawings; it can also match the hard chrome thickness an existing drawing calls for.
Can I run it on my existing line?
Hydraulic rods are coated on the continuous line, which is a new production line built by our equipment partner to Savroc's process design. It is not a conversion of an open-tank plant. Converting an existing line is possible for other applications, such as engine valves and shock absorber rods.
See it for yourself
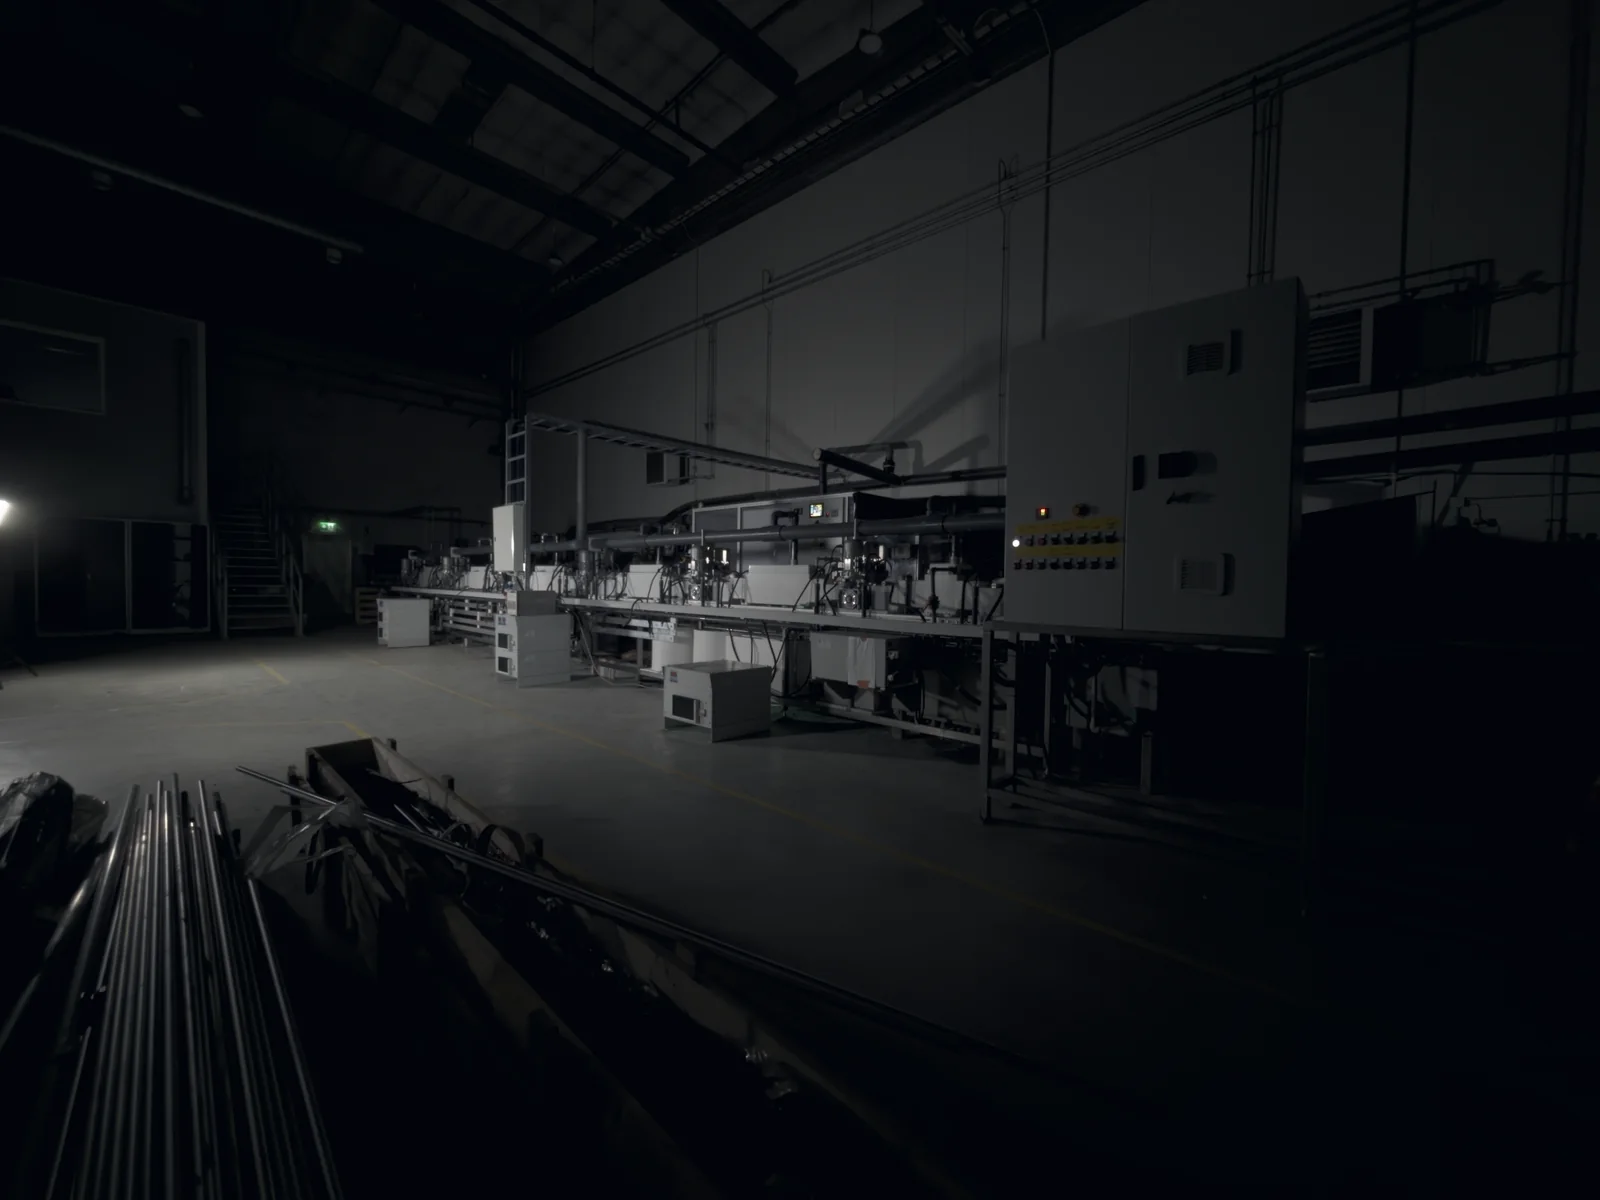
The line runs in Kuopio. Come and watch it coat a rod.
Bring your drawings or your parts. Jussi Räisä shows you the line, the test data and what a project in your plant would look like. No sales deck, no commitment.
Jussi Räisä, CEO jussi.raisa@savroc.com +358 44 307 1409